o
p
t
i
m
a
r
o
b
o
t
i
c
s
Make a Call
Make a Call
Blogs
10 Auto Pipe Welding Tips for Global Buyers
Buying Auto Pipe Welding equipment is not only a price comparison. It is a production decision involving pipe material, diameter, wall thickness, joint design, and factory conditions. A machine that performs well on stainless steel may struggle with carbon steel or narrow root gaps. Small differences matter.
John C. Lippold, a respected welding-metallurgy expert, explains a central principle: “Weldability is not simply a material property; it depends on the welding process and procedure.” This idea guides the ten tips in this article. Global buyers should examine welding current stability, torch alignment, wire feeding, shielding-gas control, and automated travel speed. They should also request sample welds, procedure records, inspection results, and clear maintenance terms from suppliers.
Look closely at the bead.
A polished brochure proves little. Ask how the system handles real pipe sections, changing wall thicknesses, imperfect fit-up, and repeated production cycles. Check whether operators can adjust parameters without creating inconsistent results. Remote support, spare-part access, training, and installation assistance also affect long-term value.
Some buyers focus too heavily on automation speed. That can be a mistake. A faster cycle is not useful if repairs increase or weld quality varies between shifts. Even experienced teams may overlook cable routing, fixture rigidity, or workshop temperature. These details deserve practical testing.
The following guide offers a buyer-focused framework for comparing Auto Pipe Welding systems. It does not promise one universal solution. Instead, it encourages careful questions, documented trials, and honest evaluation before purchase.
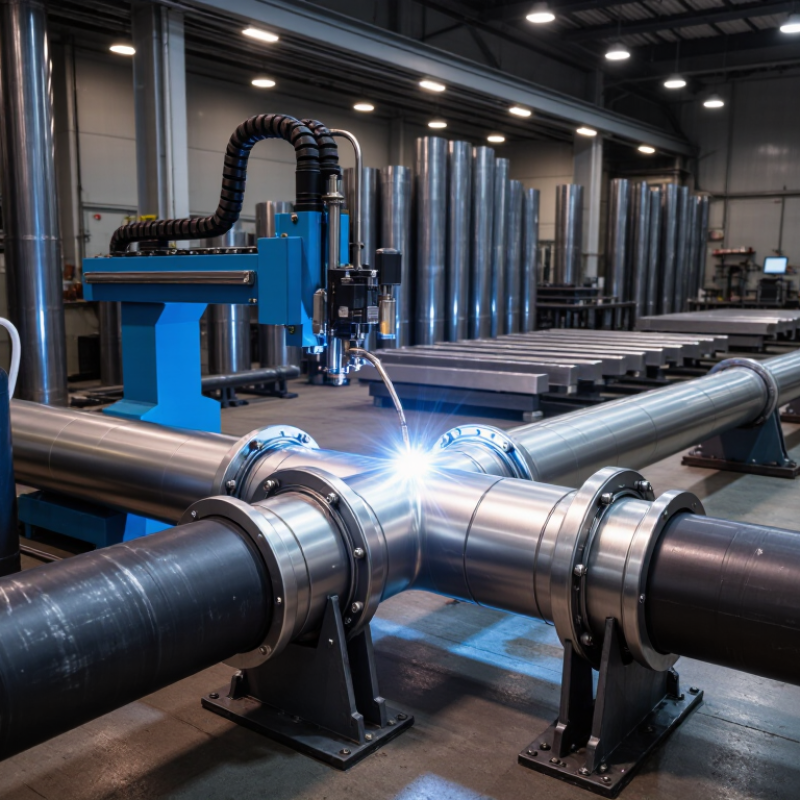
Table of Contents [Hide]
Tips 1–2: Define Pipe OD, Wall Thickness, Materials, and ISO 15614-1 WPS
Tip 1: Define the pipe OD and wall thickness before requesting an automatic welding system. A 273 mm outside diameter pipe with a 12.7 mm wall needs different tooling than a 508 mm pipe with a 6 mm wall. These dimensions affect clamping, torch travel, heat input, and weld access. Specify tolerances, ovality, joint preparation, and root gap. Do not rely on nominal size alone. ISO 15614-1 requires welding procedure qualification against defined essential variables, including thickness ranges and joint details. A rushed dimensional sheet can still mislead suppliers.
Tip 2: State the material grade and require an ISO 15614-1 qualified WPS. Carbon steel, stainless steel, duplex, and nickel alloys respond differently to heat, shielding gas, and interpass temperature. Include the exact standard, grade, delivery condition, filler classification, and preheat limits. Ask for the supporting PQR, test method, and acceptance criteria. The International Institute of Welding highlights procedure control as a major factor in repeatable weld quality. That matters when automation removes some operator correction. It does not remove engineering responsibility.
The American Welding Society’s 2023 workforce report projected a need for about 330,000 new welding professionals in the United States by 2028. Consistent documentation helps reduce dependence on scarce expert judgment. In practice, buyers should compare the proposed machine settings with the qualified WPS, then run a representative trial using real pipe dimensions. Small deviations expose weaknesses early.
Brands
Proudly Trusted by Top Suppliers Worldwide
Let us know and we will automate, together to fit your industrial needs.
 +91-97254 16844
Clients
Proudly Trusted by Top Companies Worldwide

Do you need Help? Get in touch.
X
Please fill out the form below and we will get back to you as soon as possible.