o
p
t
i
m
a
r
o
b
o
t
i
c
s
Make a Call
Make a Call
Blogs
China Best Aluminum Profile For Pergola Suppliers?
Choosing the right China Best Aluminum Profile For Pergola Suppliers? This question deserves more than a price comparison. A pergola profile must support outdoor comfort, structural stability, and a clean architectural appearance. The selected Aluminum Profile For Pergola should match the project’s span, roof system, wind exposure, drainage design, and installation method.
Experienced buyers usually examine alloy grades, wall thickness, extrusion accuracy, and surface treatment before requesting a quotation. Common options include 6063 aluminum for attractive finishes and reliable forming performance. However, alloy selection should follow engineering requirements, not habit. Powder coating quality also matters. Look for controlled pretreatment, consistent color, strong adhesion, and documented outdoor durability. A small sample can reveal uneven corners, scratches, weak coating, or poor dimensional control.
Reliable suppliers should provide drawings, tolerances, material records, inspection reports, and clear packaging details. Factory experience is useful, but it does not replace evidence. Ask how profiles are tested, measured, bundled, and protected during shipping. Photos of production lines help, although independent verification is stronger. Certifications can support credibility, yet buyers should confirm their scope and validity.
No supplier is perfect. Even a capable factory may miss a detail in a complex custom order. I have found that clear drawings and repeated sample checks prevent expensive misunderstandings. Buyers should also review communication speed, mold ownership, minimum quantities, lead times, and after-sales support. The best choice balances technical ability, transparent documentation, stable quality, and practical cooperation. A low quote may look attractive, but dependable performance usually has a longer value.
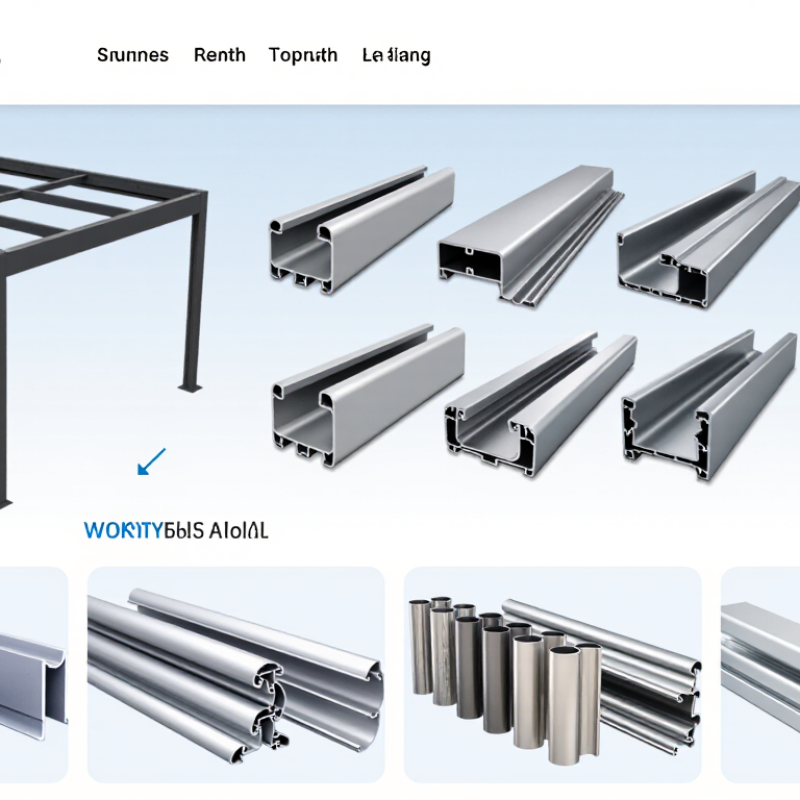
Table of Contents [Hide]
What Makes an Aluminum Profile Suitable for Pergola Construction
China Best Aluminum Profile For Pergola Suppliers?
What Makes an Aluminum Profile Suitable for Pergola Construction
A suitable aluminum profile must balance strength, weight, drainage, and appearance. Pergolas face wind, rain, sunlight, and repeated temperature changes throughout the year. Profile geometry matters more than surface shine. Deeper sections usually resist bending better. Internal ribs can improve stiffness without adding excessive material.
Experienced fabricators often prefer architectural aluminum alloys with consistent wall thickness. Uneven walls may cause weak screw connections or visible distortion. A practical design should include channels for concealed drainage. Water trapped inside the frame can create staining and installation problems. Small details matter.
Connection design deserves equal attention. Profiles should support proper brackets, fasteners, and expansion gaps. Aluminum expands in heat, so rigid joints may become stressed. Coating quality also affects long-term performance. Ask for coating specifications, alloy certificates, section drawings, and load calculations. Independent testing is more reliable than attractive product photographs.
In supplier evaluations, sample sections reveal useful facts quickly. Check cutting accuracy, corner alignment, coating consistency, and surface scratches. A polished finish can hide weak engineering. This is easy to overlook. Some projects also need custom extrusion dies, which can increase cost and lead time. A cheaper profile may demand stronger reinforcement later. That mistake is not always visible during the first installation.ಿಜೆ
China Best Aluminum Profile For Pergola Suppliers? - What Makes an Aluminum Profile Suitable for Pergola Construction
| Evaluation Dimension | Recommended Specification | Why It Matters for Pergolas | Supplier Verification Point |
|---|---|---|---|
| Primary Alloy | 6063 aluminum alloy for most architectural profiles; 6061 or 6005A where higher structural strength is required. | 6063 provides good extrudability, surface quality, corrosion resistance, and suitability for visible architectural components. | Request the alloy designation and a material certificate for each production batch. |
| Temper Condition | T5 is commonly used for extruded architectural profiles; T6 may be selected for components needing higher strength. | The temper affects yield strength, dimensional stability, machinability, and resistance to deformation. | Confirm the temper against the approved technical drawing and applicable material standard. |
| Profile Wall Thickness | Typically about 1.5–3.0 mm for non-load-bearing covers and trims; approximately 2.0–5.0 mm or more for posts, beams, and structural members, subject to engineering calculations. | Adequate wall thickness improves stiffness, screw retention, connection strength, and resistance to wind-induced movement. | Check actual wall thickness at critical sections rather than relying only on the nominal profile weight. |
| Profile Geometry | Closed or multi-chamber sections for posts and beams, with reinforced corners and integrated channels for fasteners, louvers, and drainage. | Section shape often has a greater effect on stiffness and deflection than alloy choice alone. | Ask for section properties such as area, moment of inertia, and torsional characteristics. |
| Wind Resistance | The complete pergola system should be designed for the project-specific basic wind speed, exposure, height, roof configuration, and local building requirements. | Wind uplift and lateral pressure can govern the required profile size, fasteners, anchors, and foundation design. | Require project-specific structural calculations or tested design data; do not approve profiles using alloy alone. |
| Surface Finish | Exterior-grade powder coating, commonly specified to AAMA 2604 or AAMA 2605; anodizing may be specified to the required architectural anodic coating class. | A suitable finish protects the aluminum from weathering, ultraviolet exposure, moisture, and color fading. | Verify coating thickness, pretreatment process, color tolerance, gloss, adhesion, and weathering test documentation. |
| Corrosion Protection | Use a suitable pretreatment system and isolate aluminum from incompatible metals; use corrosion-resistant stainless-steel fasteners where appropriate. | Coastal salt, standing water, and galvanic contact can accelerate corrosion at joints and fastener locations. | Request salt-spray or cyclic-corrosion test results relevant to the selected coating system and environment. |
| Dimensional Tolerance | Manufacture according to an applicable extrusion tolerance standard, such as EN 755-9 or ASTM B221 requirements where applicable. | Controlled dimensions improve fit-up, panel alignment, sealing performance, and installation efficiency. | Inspect straightness, twist, wall thickness, cut length, hole position, and profile dimensions using calibrated equipment. |
| Drainage and Water Management | Include sloped surfaces, drainage channels, weep holes, and sealed or mechanically protected joints where water may collect. | Proper drainage reduces staining, freeze-related damage, concealed corrosion, and water intrusion. | Review assembly drawings and confirm that drainage paths remain open after installation. |
| Thermal Movement | Allow for aluminum’s linear thermal expansion of approximately 23.1 × 10⁻⁶/°C through expansion joints or sliding connections where required. | Long profiles can expand and contract significantly between hot and cold conditions, causing stress or joint movement. | Confirm joint spacing, connection details, and sealant movement capability in the installation design. |
| Connection System | Use engineered corner joints, internal sleeves, stainless-steel fasteners, structural brackets, and compatible isolating washers or gaskets. | Connections transfer wind, roof, and operational loads; weak joints can undermine otherwise strong profiles. | Request connection load data, fastener specifications, torque requirements, and installation tolerances. |
| Fabrication Compatibility | Profiles should support accurate cutting, drilling, tapping, CNC machining, gasket insertion, and modular assembly without excessive distortion. | Good fabrication compatibility reduces installation time, material waste, and field adjustment. | Evaluate sample machining, cut-end quality, burr control, and repeatability before mass production. |
| Quality Documentation | Provide technical drawings, alloy and temper certificates, coating records, inspection reports, packing specifications, and traceability information. | Documented quality controls make it easier to verify consistency and manage warranty or compliance requirements. | Select suppliers able to provide batch-level traceability and samples that match production parts. |
| Sustainability and Recyclability | Prefer aluminum with documented recycled content where project requirements permit, while maintaining verified alloy, temper, and performance requirements. | Aluminum is durable and recyclable, but responsible sourcing and production documentation are needed for credible environmental claims. | Request recycled-content declarations, environmental product information, and responsible packaging details where required. |
Note: Profile dimensions, alloy temper, connection details, and wind-load requirements must be verified by a qualified structural professional for the specific pergola location and design.
Brands
Proudly Trusted by Top Suppliers Worldwide
Let us know and we will automate, together to fit your industrial needs.
 +91-97254 16844
Clients
Proudly Trusted by Top Companies Worldwide

Do you need Help? Get in touch.
X
Please fill out the form below and we will get back to you as soon as possible.