o
p
t
i
m
a
r
o
b
o
t
i
c
s

Make a Call


Make a Call
Blogs
China Best FR209E Type Coupler Body Supplier?
Choosing the China best FR209E Type Coupler Body supplier requires more than comparing unit prices. The component must withstand repeated impact, tensile loads, vibration, and harsh track conditions. A coupler body may appear simple, yet its casting quality affects fleet safety, maintenance intervals, and operating costs.
The UNIFE World Rail Market Study 2024 reports continued growth in global rail investment, driven by fleet renewal and infrastructure expansion. This trend increases demand for dependable railway components and traceable manufacturing. For buyers, supplier evaluation should include material specifications, heat-treatment records, dimensional inspection, and batch-level documentation. The AAR Manual of Standards and Recommended Practices also shows why railway components need controlled production and qualification procedures. These references do not automatically approve every Chinese factory. They provide a useful framework for asking better questions.
An experienced supplier of Fr209e Type Coupler Body should demonstrate pattern control, certified material testing, and consistent machining accuracy. Ask for tensile results, hardness values, chemical composition, and non-destructive testing records. Request samples before approving mass production. Inspect the coupler body around the shank transition, draft gear interface, and high-stress fillets. Small surface defects can become expensive failures.
Price still matters. It should not lead.
China offers strong casting capacity, competitive engineering support, and flexible production volumes. However, supplier claims may be incomplete, and inspection reports can vary in quality. A practical sourcing decision combines factory audits, independent testing, production references, and clear acceptance criteria. The best supplier is not simply the cheapest option. It is the manufacturer that can repeatedly deliver a compliant Fr209e Type Coupler Body, with evidence that survives technical review.
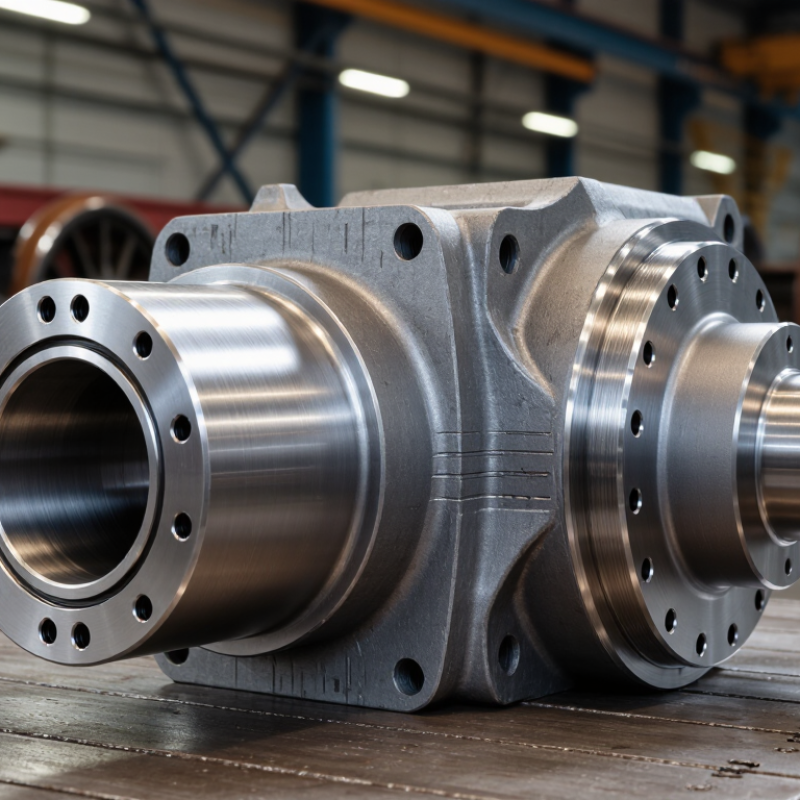
Table of Contents [Hide]
What Is an FR209E-Type Coupler Body?
An FR209E-type coupler body is the main structural housing of a railway vehicle coupler. It transfers pulling and pushing forces between connected cars. Made from high-strength steel, it surrounds the working cavity for the knuckle, lock, and related parts. The body must resist impact, repeated loading, and alignment errors during service. Small dimensions matter. The designation should be checked against the purchaser’s drawing and applicable railway standard.
A reliable supplier should control material selection, casting or forging, heat treatment, and dimensional inspection. Ultrasonic testing can help identify internal flaws, while surface checks reveal cracks, sharp transitions, or poor finishing.
Critical areas include the coupler head, shank connection, draft gear seat, and mounting surfaces. Each area needs suitable measuring tools. A supplier with traceable inspection records can explain the steel grade, heat-treatment results, and test methods clearly.
The term FR209E may not describe every detail of one production drawing. That point is easy to overlook. Before ordering, compare the body profile, mounting geometry, tolerances, and inspection requirements. A visually similar body may still fit poorly or experience uneven loading. Practical experience also shows that packaging deserves attention, because exposed machined surfaces can corrode during transport. The best purchasing decision comes from technical documents, sample verification, and open communication with the manufacturer.
Brands
Proudly Trusted by Top Suppliers Worldwide







Let us know and we will automate, together to fit your industrial needs.
 +91-97254 16844
Clients
Proudly Trusted by Top Companies Worldwide


Do you need Help? Get in touch.
X
Please fill out the form below and we will get back to you as soon as possible.