o
p
t
i
m
a
r
o
b
o
t
i
c
s
Make a Call
Make a Call
Blogs
China Best Conical Burr Hand Grinder Manufacturer?
Choosing the right Conical Burr Hand Grinder manufacturer is about more than comparing prices or polished product photos. A good grinder should feel steady in the hand, turn smoothly, and produce grounds suited to the brewing method. Small details matter: burr alignment, adjustment steps, handle comfort, and how easily coffee residue can be cleaned away. A sample can reveal more than a catalog.
This guide explores what buyers can examine when assessing manufacturers in China, including materials, production capabilities, quality checks, customization, and communication. Useful evidence may include clear specifications, inspection records, sample testing, and consistent answers to practical questions. Ask how the burrs are made and checked, whether replacement parts are available, and how the grinder performs across different settings. Details count.
No single supplier is automatically the best fit for every brand or buyer. A compact model may suit travel, while a heavier body can feel more stable on a kitchen counter. Even then, weight alone proves little. I would compare samples and test them with the same beans before making a decision; that takes time, but it can expose uneven adjustment or an uncomfortable grip. Supplier claims deserve verification. By focusing on observable product performance and transparent manufacturing information, readers can make a more grounded shortlist and avoid choosing on appearance alone.
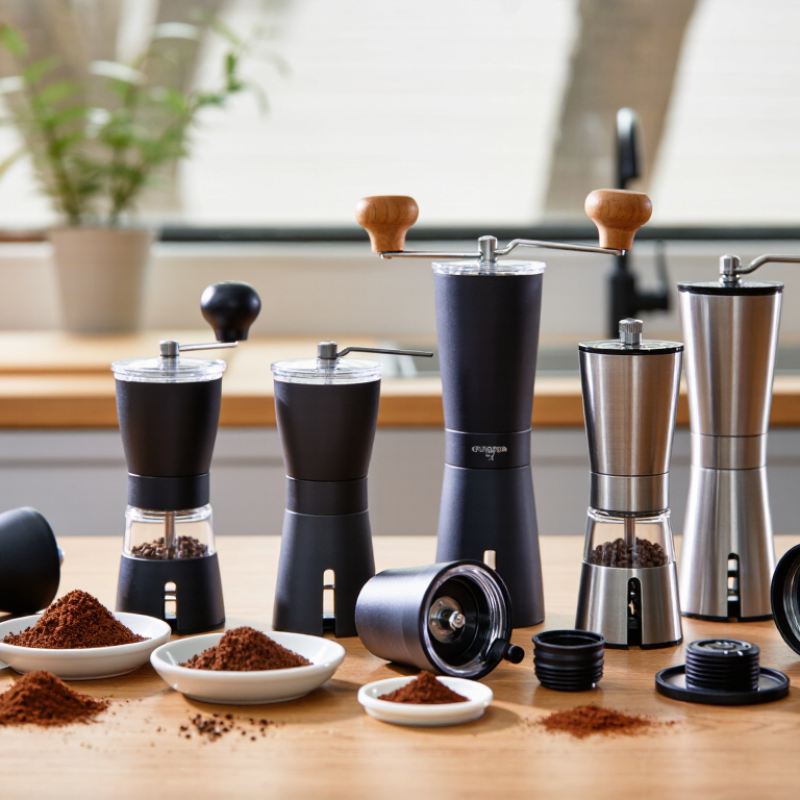
Table of Contents [Hide]
What Defines a Conical Burr Hand Grinder?
What Defines a Conical Burr Hand Grinder?
A conical burr hand grinder uses two cone-shaped burrs to crush coffee beans into smaller particles. One burr usually sits inside the other. As you turn the handle, the beans travel through the narrowing gap and are ground. The gap setting controls particle size: a wider space suits many French press brews, while a tighter one supports espresso-style preparation. Results also depend on burr alignment, bean condition, and how steadily you turn the handle. No grinder setting works perfectly for every coffee.
Good grinders feel stable in the hand and allow repeatable adjustments. Look for a handle that turns without wobbling, clear grind settings, and burrs that are easy to clean. A few coarse particles may remain, especially with light-roasted beans. That can be frustrating. Still, grind consistency is only one part of a good cup; water temperature and brewing time matter too.
Tips: Change one setting at a time, then brew and taste. Keep notes on the setting and brew time. Brush away loose grounds after use, and avoid washing burrs unless the maker’s care instructions allow it. Small changes reveal more than guesswork.
Brands
Proudly Trusted by Top Suppliers Worldwide
Let us know and we will automate, together to fit your industrial needs.
 +91-97254 16844
Clients
Proudly Trusted by Top Companies Worldwide

Do you need Help? Get in touch.
X
Please fill out the form below and we will get back to you as soon as possible.