o
p
t
i
m
a
r
o
b
o
t
i
c
s
Make a Call
Make a Call
Blogs
China Best Galvanized Self Drilling Screws Manufacturer?
Choosing China’s best manufacturer of Galvanized Self Drilling Screws takes more than comparing prices or catalogue photos. These fasteners must drill through the specified material, form a dependable thread, and resist corrosion in real service conditions. A screw that looks consistent in a sample box may perform differently across a large production batch. Small details matter.
The market context is substantial. Grand View Research’s Fasteners Market Size, Share & Trends Analysis Report estimated the global fasteners market at USD 90.7 billion in 2023 and projected a 4.5% compound annual growth rate from 2024 to 2030. This broad figure covers many fastener types, not galvanized self-drilling screws alone. Still, it reflects demand across sectors where reliable fastening supports construction and manufacturing. It should be treated as context, not proof that any single supplier is qualified.
For buyers, a useful comparison starts with the application: base-metal thickness, head style, point design, coating specification, and exposure conditions. Then review documented inspection procedures, material traceability, sample testing, and consistency between samples and production orders. Ask how coating thickness and drilling performance are checked. Request records. Verify the details.
No coating suits every environment, and a low unit price may hide costs from rework or premature corrosion. Manufacturer claims deserve careful review; independent test evidence is more persuasive. The strongest shortlist is built on verifiable specifications, responsive technical support, and repeatable quality—not a single “best” label. There is room for judgment, too. A capable supplier should explain where its product fits, and where it does not.
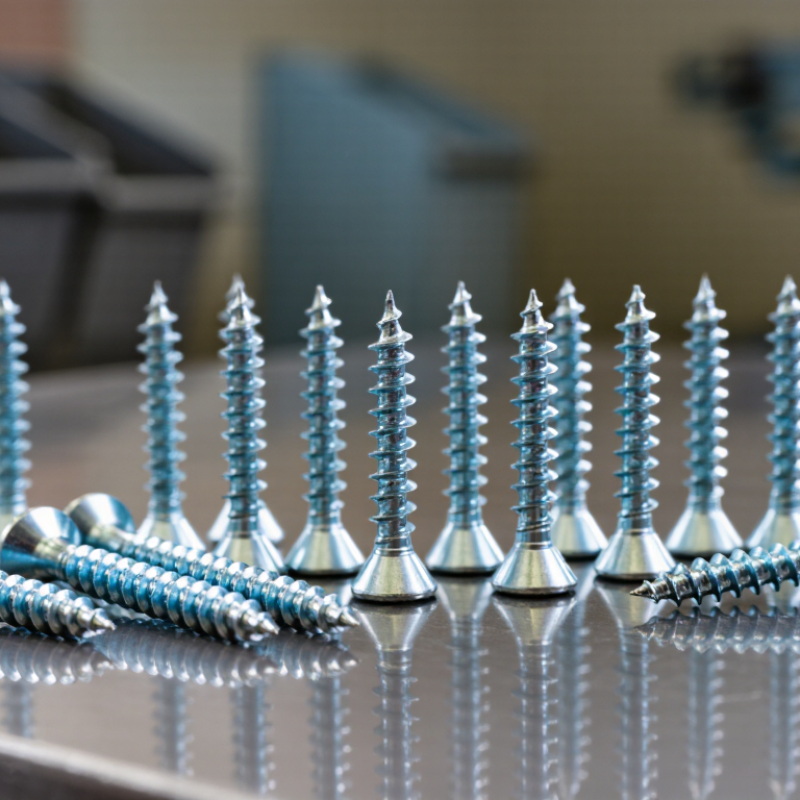
Table of Contents [Hide]
What Are Galvanized Self-Drilling Screws?
China Best Galvanized Self Drilling Screws Manufacturer?
What Are Galvanized Self-Drilling Screws?
Galvanized self-drilling screws are fasteners with a zinc-coated surface and a drill-shaped point. The point cuts through suitable materials, often removing the need to drill a pilot hole. Their threads then grip the material as the screw is driven. A time-saver, when chosen correctly.
The zinc coating helps slow corrosion by creating a protective barrier. Some coatings can also provide sacrificial protection if the surface is scratched, though performance depends on coating type and thickness. Galvanized finishes vary, so “galvanized” alone does not tell you how long a screw will last in a specific environment. That detail matters.
These screws are commonly used to fasten sheet metal to compatible supports, but not every screw suits every material or thickness. Check the manufacturer’s specifications for drilling capacity, coating, and recommended installation conditions. Use a steady driver and stop when the head is seated; overdriving can damage the coating or the material. A small test installation can reveal problems before a full job begins. It is easy to assume one screw will do it all. Usually, that assumption needs checking.
Brands
Proudly Trusted by Top Suppliers Worldwide
Let us know and we will automate, together to fit your industrial needs.
 +91-97254 16844
Clients
Proudly Trusted by Top Companies Worldwide

Do you need Help? Get in touch.
X
Please fill out the form below and we will get back to you as soon as possible.