o
p
t
i
m
a
r
o
b
o
t
i
c
s
Make a Call
Make a Call
Blogs
Best China PVC 2-Piece Ball Valve Supplier?
Choosing the best China PVC 2-Piece Ball Valve supplier requires more than comparing catalog prices. The right partner should demonstrate material knowledge, consistent production, reliable testing, and clear technical communication. A polished website is helpful. It is not proof.
As thermoplastics piping consultant John L. McCready says, “A valve is only reliable when its materials, design, installation, and service conditions agree.” This practical view matters on real projects. A valve installed beside a chemical dosing skid may face corrosion, pressure changes, frequent cycling, and limited maintenance access. Its body, seals, stem, and connection method must suit those conditions.
Look for suppliers that identify PVC grades, sealing materials, pressure ratings, temperature limits, and applicable test procedures. Ask for dimensional drawings, sample inspection records, batch traceability, and evidence of pressure testing. Small details matter. A stiff handle may signal poor assembly. Uneven molding can reveal process weakness. Leaking seats are unacceptable.
Experience also matters during selection. A capable supplier will ask about media, flow requirements, pipe standards, installation position, and operating frequency. They should explain limitations instead of promising universal compatibility. That honesty builds trust.
No supplier is perfect. Even experienced factories can face inconsistent batches, delayed communication, or packaging damage. The better question is whether problems are detected, documented, and corrected quickly. This guide compares China-based manufacturers through that practical lens, helping buyers evaluate product quality, technical support, customization, export capability, and long-term value before placing an order.
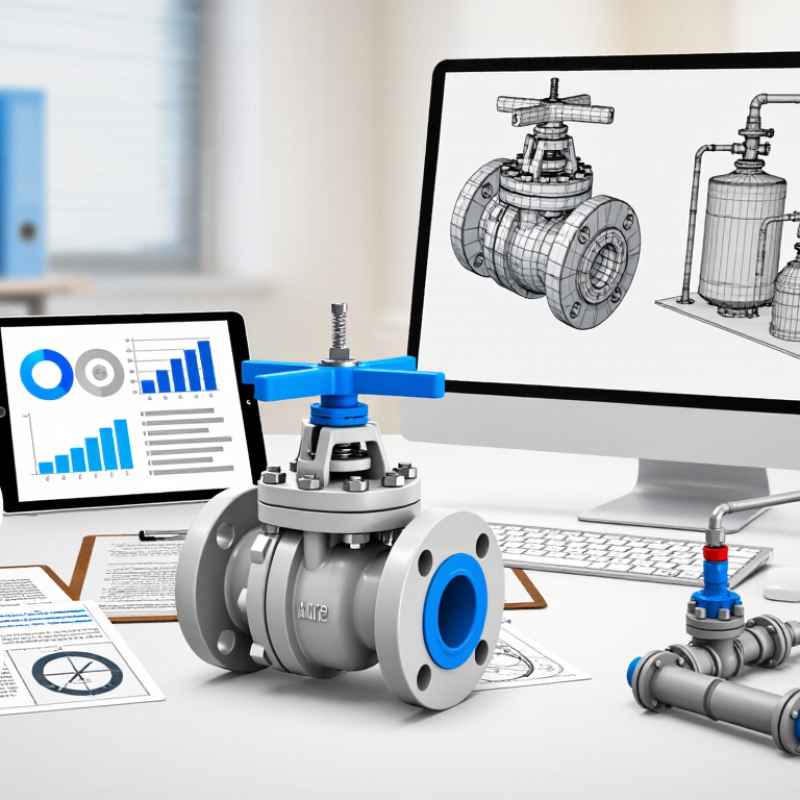
Table of Contents [Hide]
What Is a PVC 2-Piece Ball Valve?
A PVC 2-piece ball valve controls liquid flow with a quarter-turn handle. Inside, a drilled plastic ball rotates between two sealing seats. When the hole aligns with the pipe, fluid passes through. Turning the handle 90 degrees blocks the passage.
The “2-piece” design means the valve body has two main sections joined during assembly. This structure can simplify production and inspection. However, it does not always mean every part is replaceable in service. PVC offers good corrosion resistance for water, irrigation, and many compatible chemicals. Temperature, pressure, fluid concentration, and connection type still require careful checking. Socket, threaded, and flanged ends suit different installation conditions. A reliable supplier should provide clear pressure ratings, material data, dimensional drawings, and batch inspection records. Small details matter. An incorrectly selected seal can fail earlier than expected.
Tips: Confirm the medium before ordering. Check maximum working temperature and pressure together, not separately. Avoid forcing the handle beyond its normal quarter-turn. Support nearby pipes to reduce stress on the valve body. During installation, clean pipe ends and allow solvent cement to cure fully. “Maintenance-free” sounds convenient, but it deserves caution; seals can age, and poor alignment may cause leakage. A practical inspection should include handle movement, joint condition, and signs of chemical attack.
Brands
Proudly Trusted by Top Suppliers Worldwide
Let us know and we will automate, together to fit your industrial needs.
 +91-97254 16844
Clients
Proudly Trusted by Top Companies Worldwide

Do you need Help? Get in touch.
X
Please fill out the form below and we will get back to you as soon as possible.