o
p
t
i
m
a
r
o
b
o
t
i
c
s
Make a Call
Make a Call
Blogs
How to Choose the Best Food Sealer Machine for Your Business
Choosing the right Food Sealer Machine can determine whether a product reaches customers fresh, secure, and visually appealing. It also affects labor costs, packaging waste, shelf life, and daily production speed. A busy kitchen needs different equipment from a frozen-food factory. That difference matters.
PMMI’s 2024 State of the Industry report identifies food and beverage as major users of packaging machinery. Its findings also highlight continuing investment in automation, labor efficiency, and flexible production lines. Grand View Research reports that the global food packaging market is expanding as convenience foods, e-commerce, and longer shelf-life demands increase. These trends create opportunity, but they can also encourage rushed purchasing decisions.
Food-packaging expert Dr. Gordon L. Robertson offers a useful principle: “Packaging is a means of protecting food from external influences.” Protection is not limited to sealing strength. It includes oxygen control, moisture resistance, temperature tolerance, and consistent closure quality. A weak seal may look acceptable under showroom lighting. It can fail after vibration, refrigeration, or repeated handling.
The best Food Sealer Machine should match your packaging material, product moisture, pouch size, output target, and cleaning routine. Vacuum sealing may suit meat or prepared meals. Continuous band sealing may better support dry goods and high-volume operations. Modified-atmosphere systems require more technical control.
Do not trust speed claims alone. Ask for seal samples using your actual product. Measure cycle time, reject rates, noise, cleaning effort, and energy use. A perfect machine does not exist. The most expensive option may still be wrong for your workflow. This guide explains how to compare equipment carefully, using practical evidence rather than attractive specifications.
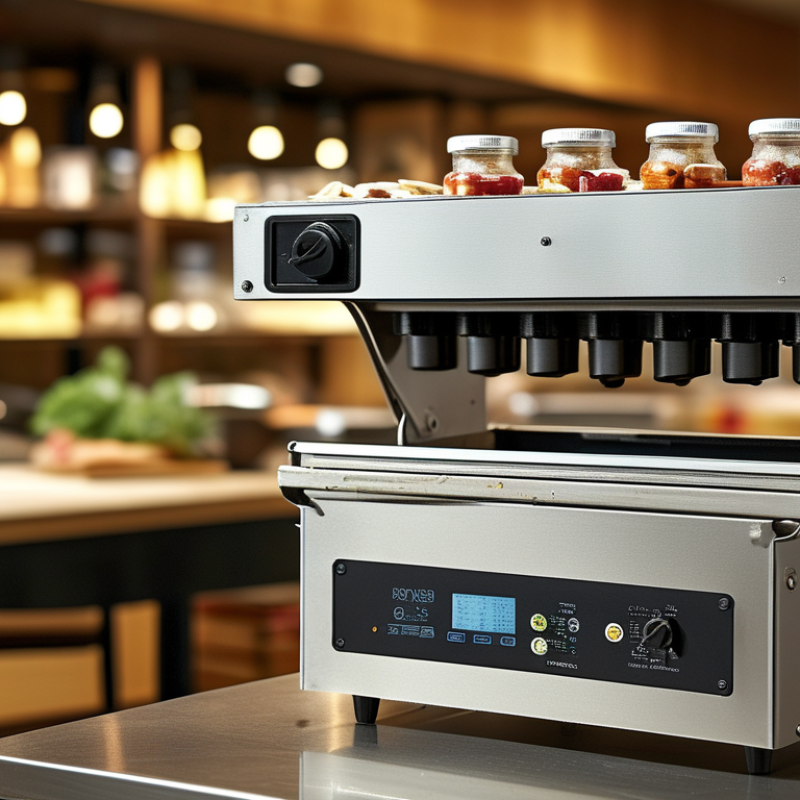
Table of Contents [Hide]
Define Product and Packaging Needs Using FDA Food Code’s 41°F Standard
How to Choose the Best Food Sealer Machine for Your Business
Define Product and Packaging Needs Using FDA Food Code’s 41°F Standard
Before choosing a food sealer machine, measure how your products behave at 41°F or below. The FDA Food Code uses 41°F as the cold-holding limit for many refrigerated foods. A sealer cannot correct unsafe cooling or storage. It only protects the package after proper temperature control.
Start with product details. Fresh meat may release liquid, while soups create pressure and spills. Delicate pastries need gentle sealing. A chamber-style machine may suit liquid foods better than an external suction model. Check seal width, bag thickness, production speed, and cleaning access. Small details matter.
Keep a calibrated thermometer nearby. Record product temperature before sealing, after sealing, and during storage. The packaging may look perfect.
Reduced-oxygen packaging requires extra care. Vacuum sealing can change how certain foods support bacterial growth. Your food safety plan may need specific controls, monitoring, and staff training. Requirements can vary because local authorities may adopt different versions of the FDA Food Code. Confirm the applicable rules before selling sealed products.
A common mistake is selecting equipment by motor power alone. That assumption needs challenging. Test real products, not empty bags. Watch for weak seals, trapped liquid, and damaged film after refrigeration. Recheck the process when recipes, portion sizes, or packaging materials change. A reliable machine fits both your product and your temperature-control system.
Brands
Proudly Trusted by Top Suppliers Worldwide
Let us know and we will automate, together to fit your industrial needs.
 +91-97254 16844
Clients
Proudly Trusted by Top Companies Worldwide

Do you need Help? Get in touch.
X
Please fill out the form below and we will get back to you as soon as possible.