o
p
t
i
m
a
r
o
b
o
t
i
c
s
Make a Call
Make a Call
Blogs
How to Choose Aluminum Tube Extrusions for Your Project?
Choosing Aluminum Tube Extrusions is a design decision, not merely a purchasing task. The right tube must carry loads, manage heat, resist corrosion, and fit the production process. Wall thickness, alloy, temper, diameter, and tolerance all matter. A tube that looks efficient on paper may twist during cutting or deform during assembly.
Industry data shows why this choice deserves care. The Aluminum Association’s 2024 Aluminum Statistical Review describes aluminum as a major material across transportation, construction, packaging, and electrical applications. Grand View Research also projects continued growth in the global aluminum extrusion market, driven by lightweight vehicle structures, renewable-energy equipment, and efficient building systems. These reports indicate strong demand, but they do not remove project-specific risks. Market growth is not a substitute for engineering validation.
Jeff Henderson, former president of the Aluminum Extruders Council, has emphasized, “Good extrusion design begins with understanding the application.” That principle is easy to overlook. A 6063 tube may provide an attractive finish and smooth extrusion performance, while 6061 may offer higher strength but require different fabrication choices. Consider a 40-millimeter tube supporting a vibrating frame. Its alloy alone cannot predict performance; joint design, unsupported length, surface treatment, and fatigue exposure also matter.
Small details decide outcomes.
This guide explains how to compare Aluminum Tube Extrusions by performance, manufacturability, cost, and application demands. It also questions common assumptions, because the cheapest profile can become expensive after machining, rework, or premature replacement. Validate the selection with supplier data, drawings, and practical testing.
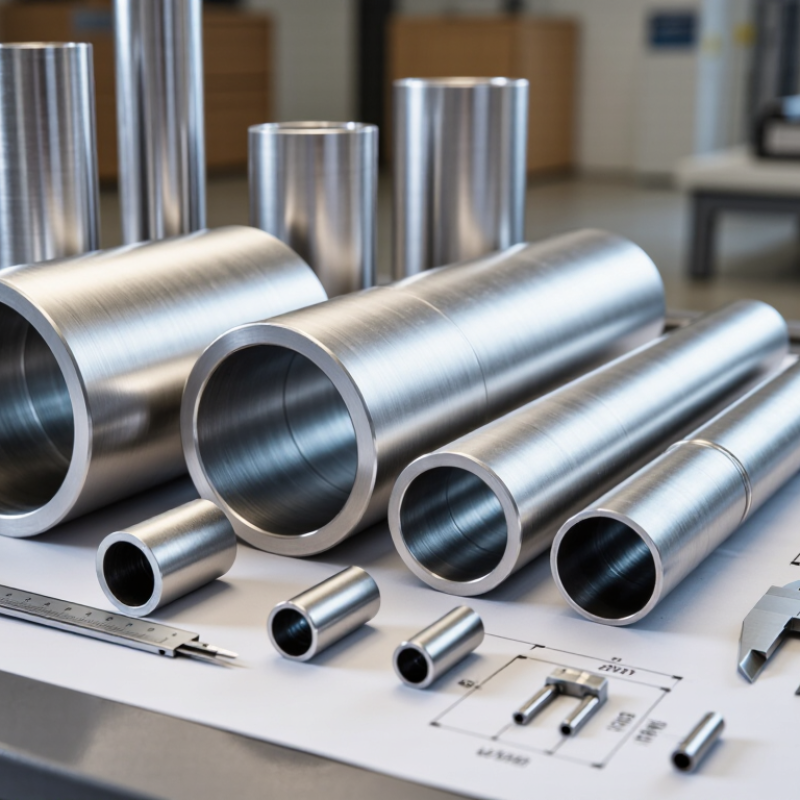
Table of Contents [Hide]
Define Project Requirements and Tube Performance Goals
Before choosing an aluminum tube extrusion, translate the project into measurable requirements. Record the outer dimensions, wall thickness, tube length, connection method, and expected load. A tube supporting a 40-kilogram instrument needs a different design from one protecting lightweight wiring. Include bending, torsion, vibration, temperature, and impact conditions. These details often expose weak assumptions early.
Material selection follows performance goals. Common 6000-series alloys offer a practical balance of strength, corrosion resistance, and extrudability. Temper also matters. A heat-treated T6 tube may improve strength, but it can complicate forming and increase cost.
Refer to ASTM B221 for extrusion requirements, while checking dimensional tolerances with the supplier. Small variations can affect sliding fits and sealing surfaces. Measure twice.
Environmental targets deserve equal attention. The International Aluminium Institute reports that recycling aluminum uses about 5% of the energy required for primary production, representing up to 95% energy savings.
Specify recycled content when it supports the project’s life-cycle goals, but verify certification and actual material availability. Surface finish, anodizing, or powder coating should match exposure conditions, not appearance alone. In coastal air, neglected protection may fail sooner than expected. That possibility needs testing.
Prototype the tube under realistic loads. Check deflection, joint movement, and heat buildup after assembly. Finite-element analysis can guide decisions, but it cannot replace physical testing.
A thinner wall may reduce weight and material use, yet it can create local buckling around drilled holes. That trade-off is easy to underestimate.
Review the design with an extrusion specialist before locking the die and production quantities.
Brands
Proudly Trusted by Top Suppliers Worldwide
Let us know and we will automate, together to fit your industrial needs.
 +91-97254 16844
Clients
Proudly Trusted by Top Companies Worldwide

Do you need Help? Get in touch.
X
Please fill out the form below and we will get back to you as soon as possible.