o
p
t
i
m
a
r
o
b
o
t
i
c
s
Make a Call
Make a Call
Blogs
How to Choose the Right Control Valve?
Selecting the right Control Valve is rarely a simple catalog decision. It affects process stability, energy use, safety, and maintenance costs.
Grand View Research reported that the global control valves market was valued at approximately USD 7.7 billion in 2023. Its analysis also expects continued growth through 2030, driven by chemical processing, power generation, water treatment, and oil and gas applications. These figures show strong demand, but market growth does not guarantee the right valve for every plant. A valve that performs well on a clean-water line may fail quickly in abrasive slurry.
The practical choice begins with process evidence. Record flow rate, pressure drop, temperature, fluid density, viscosity, and required shutoff class. Check cavitation risk, flashing, corrosion, and noise before comparing suppliers. IEC 60534 and ISA 75 standards provide widely recognized methods for sizing and testing control valves. They help engineers move beyond guesswork. Still, standards cannot replace field experience. A damaged seat, unstable actuator, or poorly tuned positioner may reveal conditions missing from the design sheet.
A neat spreadsheet can still mislead. It is worth questioning every assumption.
Reports from the International Energy Agency continue to emphasize industrial efficiency and dependable process operation. This makes valve selection more than a purchase decision. It becomes part of long-term asset management. The best Control Valve balances controllability, materials, actuator performance, diagnostics, lifecycle cost, and service support. That balance may look less impressive than the cheapest quotation, but it usually performs better beside a hot pipe, during a pressure surge, or after years of maintenance.
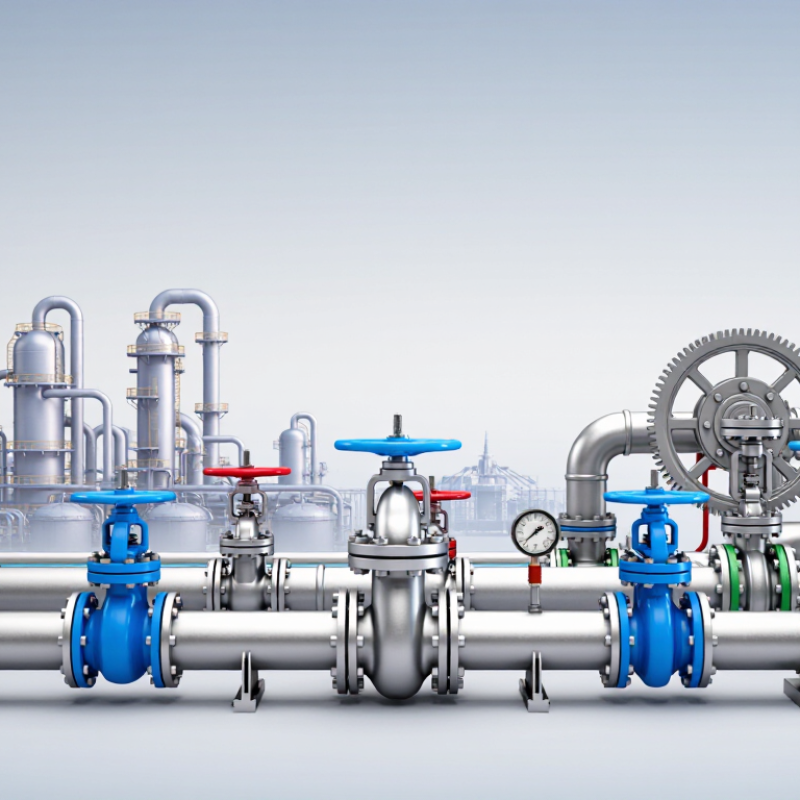
Table of Contents [Hide]
Define Process Duty: Flow, Pressure, Temperature, and Fluid Properties
Choosing the right control valve starts with defining the process duty, not selecting a valve by line size. Record the normal, minimum, and maximum flow rates. A valve that controls well at normal flow may become unstable during startup.
Pressure data needs equal care. Note inlet pressure, outlet pressure, and available pressure drop at each operating condition. A small pressure drop can limit control authority, while excessive drop may cause cavitation, noise, or flashing. I have seen calculations fail because operators supplied normal pressure instead of the real minimum value.
Temperature affects body materials, seals, and actuator performance. Record both continuous and upset temperatures. Fluid properties matter just as much. Density and viscosity influence sizing, while solids can damage trim or block narrow passages. Corrosive fluids may require compatible wetted materials. For steam, gas, or liquid service, the sizing method is different. Do not treat them as interchangeable.
A clear duty sheet should include flow units, pressure units, temperature ranges, fluid composition, and expected operating hours. Check whether the valve will throttle continuously or move only occasionally. That detail changes the wear assessment. Safety requirements also deserve attention, including the required failure position and response time. A tidy spreadsheet can still be wrong. Verify the figures with plant operators and compare them with measured conditions before final sizing.
Brands
Proudly Trusted by Top Suppliers Worldwide
Let us know and we will automate, together to fit your industrial needs.
 +91-97254 16844
Clients
Proudly Trusted by Top Companies Worldwide

Do you need Help? Get in touch.
X
Please fill out the form below and we will get back to you as soon as possible.