o
p
t
i
m
a
r
o
b
o
t
i
c
s
Make a Call
Make a Call
Blogs
What Is a Top China Ceramic Laser Reflectors Supplier?
Choosing a top China supplier for Ceramic Laser Reflectors requires more than comparing prices or polished product photographs. These components guide laser energy, endure heat, and influence system stability. A reliable supplier should demonstrate practical experience with alumina ceramics, reflective coatings, and precision machining. Their technical team should understand wavelength requirements, surface finish, dimensional tolerance, and thermal cycling performance.
Look for evidence, not promises. Ask for material certificates, inspection records, coating data, and production samples. A serious manufacturer can explain reflectance testing at your operating wavelength. They should also describe how they control flatness, edge quality, and coating adhesion. Clear communication matters. So does traceability.
Factory capability is another important signal. Visit photos may show modern equipment, but process details reveal more. Check whether the supplier uses controlled sintering, calibrated measuring tools, and documented quality procedures. Request samples from regular production, not specially prepared pieces. Compare their dimensions under consistent conditions. Small differences can affect alignment inside a laser cavity.
No supplier is perfect. Even experienced manufacturers may face coating variation, delivery pressure, or design misunderstandings. That is why a dependable partnership includes corrective action and honest technical discussion. A supplier willing to acknowledge limitations often deserves closer attention. In this guide, we examine China-based manufacturers through quality evidence, engineering competence, communication, and long-term reliability. The goal is not to select the cheapest source. It is to identify a capable partner for stable, repeatable laser performance.
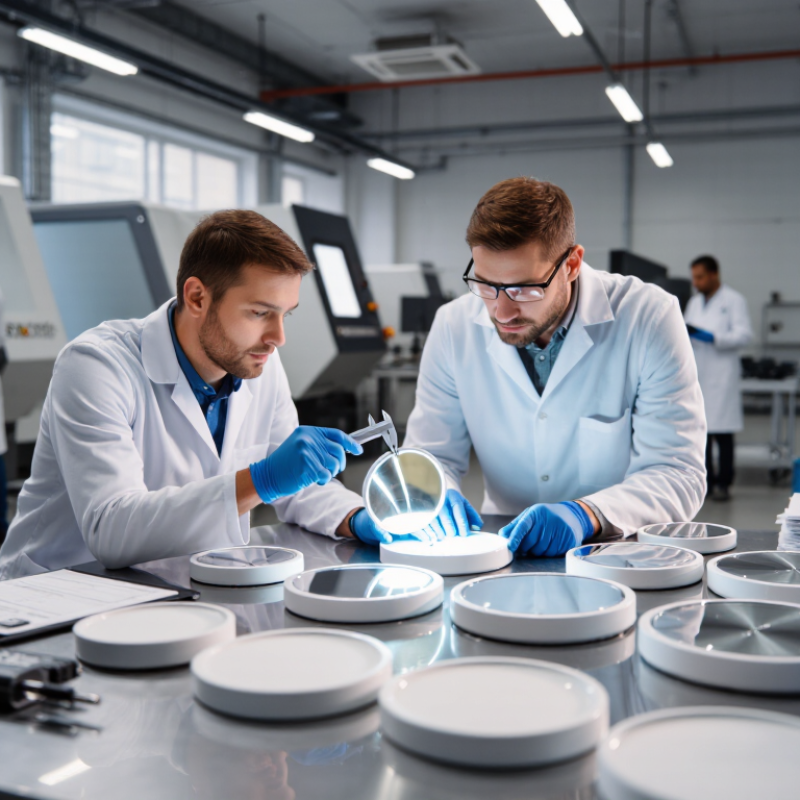
Table of Contents [Hide]
Ceramic Laser Reflectors: 99%+ Reflectivity at 1064 nm
What Is a Top China Ceramic Laser Reflectors Supplier?
Ceramic laser reflectors designed for 1064 nm systems can achieve 99% or higher reflectivity under controlled test conditions. This figure matters in Nd:YAG laser assemblies, where small optical losses may increase heat and reduce pumping efficiency. A reliable supplier should explain the test wavelength, incidence angle, surface condition, and measurement equipment behind the result. Without these details, “99%+” remains an attractive but incomplete claim.
In practical production, reflector performance depends on more than polished ceramic surfaces. Material purity, pore control, dimensional accuracy, and thermal stability all affect service consistency. Experienced manufacturers usually inspect flatness, diameter, coating adhesion, and reflectivity across several sample points. They should also provide inspection records and discuss batch-to-batch variation honestly. Some suppliers offer impressive laboratory data but provide limited evidence for continuous production. That deserves careful questioning.
A strong China-based supplier should understand custom cavity dimensions, mounting pressure, cooling conditions, and 1064 nm operating environments. Clear drawings, traceable samples, and responsive technical communication reveal genuine expertise. I would ask for a small evaluation batch before placing a large order. It may expose edge chipping, uneven surfaces, or unexpected reflectivity loss after thermal cycling. Perfection is rarely automatic. Careful verification still matters.
Brands
Proudly Trusted by Top Suppliers Worldwide
Let us know and we will automate, together to fit your industrial needs.
 +91-97254 16844
Clients
Proudly Trusted by Top Companies Worldwide

Do you need Help? Get in touch.
X
Please fill out the form below and we will get back to you as soon as possible.