o
p
t
i
m
a
r
o
b
o
t
i
c
s

Make a Call


Make a Call
Blogs
Why Choose Metal Snaps for Global Sourcing?
Why Choose Metal Snaps for Global Sourcing?
Global apparel sourcing often depends on details that buyers notice only after failure. Metal Snaps are one of those details. They must open smoothly, close firmly, and remain attractive after repeated washing. A weak cap can damage fabric. A poor finish can leave dark marks on a pale jacket.
David S. Birnbaum, a longtime apparel sourcing consultant, offers a useful principle: “The smallest component can determine the value of the finished garment.” This idea fits Metal Snaps closely. Their performance depends on alloy quality, spring tension, plating thickness, and installation pressure. A sourcing team should request production samples, not only showroom samples. Test pieces can reveal loose rings, uneven color, sharp edges, or inconsistent closure force. Small defects matter.
Global purchasing also brings practical challenges. Buyers must compare minimum order quantities, tooling charges, packaging standards, and delivery schedules. They should review factory records and confirm material specifications. Salt-spray testing may help assess corrosion resistance. Pull testing can show whether a snap will survive real use. Carton labels and batch numbers improve traceability across long supply chains.
Still, no checklist guarantees a perfect result. A polished sample can mislead. Even experienced teams sometimes overlook fabric thickness or washing conditions. That is worth admitting. The better approach combines supplier experience, documented testing, and honest review. When these steps work together, Metal Snaps become more than decorative hardware. They support durability, product consistency, and buyer confidence in international sourcing.
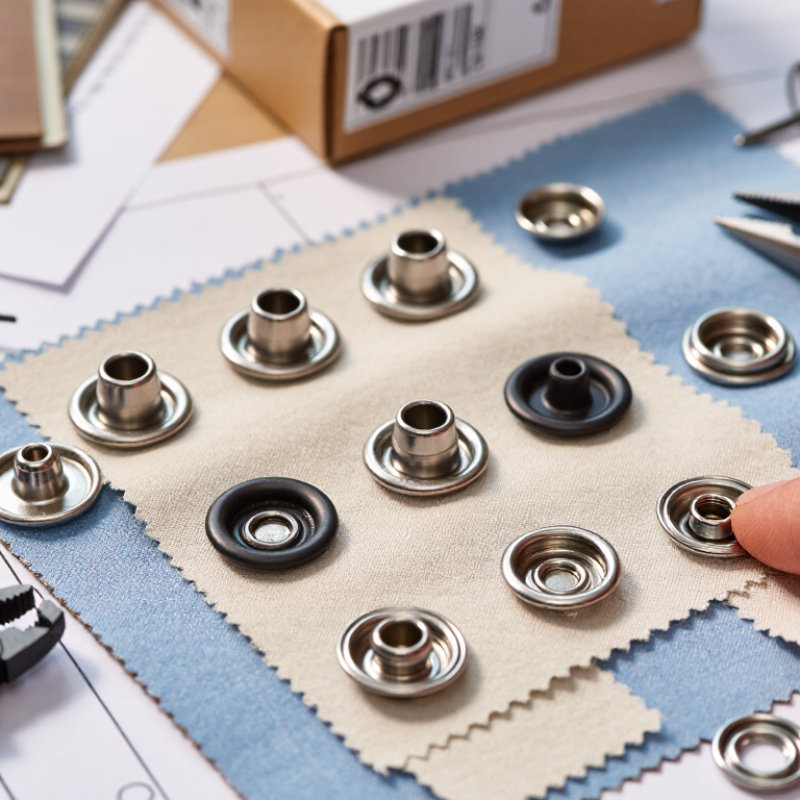
Table of Contents [Hide]
Metal Snaps Defined: Four-Part Fasteners for Apparel and Equipment
Why Choose Metal Snaps for Global Sourcing?
Metal snaps are four-part fasteners: a cap, socket, stud, and open ring. Together, they create a compact closure for jackets, workwear, bags, tents, and equipment covers. The socket receives the stud, while the ring locks the assembly through fabric or webbing. Four parts. One action.
A sourcing review should check more than appearance. Suppliers need consistent dimensions, clean forming, secure plating, and documented pull-off and corrosion tests. In production, a snap may fail because the ring cuts fabric, not because the metal breaks. Fit matters. Sampling should include repeated opening cycles, washing, humidity exposure, and installation with the intended fabric thickness. ASTM and ISO test methods can support comparable results, but test conditions must match real use.
Textile Exchange’s Materials Market Report 2024 recorded global fiber production at about 124 million tonnes in 2023, with projections approaching 160 million tonnes by 2030. That scale increases pressure to reduce replacement waste and improve component traceability. Metal snaps can support longer product use, but metal is not automatically sustainable. Buyers should request alloy details, coating information, recycled content evidence, and restricted-substance declarations. Global sourcing also needs clear tolerances and inspection records. A cheaper snap can become expensive after field returns. Sometimes, the overlooked ring causes the problem.
Brands
Proudly Trusted by Top Suppliers Worldwide







Let us know and we will automate, together to fit your industrial needs.
 +91-97254 16844
Clients
Proudly Trusted by Top Companies Worldwide


Do you need Help? Get in touch.
X
Please fill out the form below and we will get back to you as soon as possible.